Computerized Stitching Machines for Footwear Manufacturing: Types, Efficiency and Applications
Computerized stitching has become an important technology in footwear manufacturing because it can improve stitching consistency, repeatability and production efficiency.
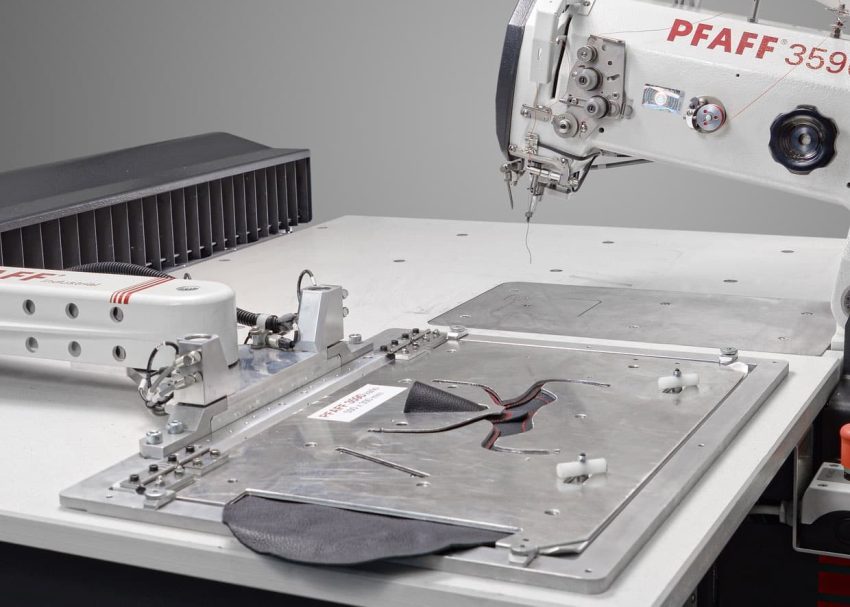
Unlike conventional sewing, where the operator controls most of the material movement manually, a computerized machine can follow a programmed sewing path and automatically perform defined sewing operations.
However, computerized stitching machines are not one single type of machine. They range from relatively compact programmable pattern machines for small components to larger machines capable of handling several components in one sewing area. Higher levels of automation can also introduce multiple pallets, automatic workpiece handling and robotic material movement.
For footwear manufacturers, the important question is therefore not simply which computerized machine is fastest. The better question is:
Which machine configuration matches the footwear component, sewing pattern, production volume, operator method and required level of automation?
Small-Area Programmable Pattern Machines
The first level of computerized stitching is the programmable pattern sewing machine. These machines are suitable when a particular footwear component requires a repeatable stitching pattern within a relatively small area. The operator positions the component in a fixture, selects or starts the programmed pattern, and the machine controls the programmed sewing movement.
A useful example is the Brother BAS-326H. Brother describes this as a direct-drive programmable electronic pattern sewer, with configurations including a 220 × 100 mm sewing area. It incorporates an LCD touch panel, digital tension and thread-break detection.
This type of machine is suitable for operations such as:
- reinforcement stitching;
- small overlays;
- tabs and straps;
- decorative patterns;
- small footwear components;
- repeated stitch geometries.
The main advantage is repeatability. Once the sewing program and fixture are correctly developed, the machine can reproduce the same stitching path repeatedly.
Medium-Area Computerized Stitching Machines
When the component requires a larger sewing envelope, a medium-area computerized machine becomes more appropriate.
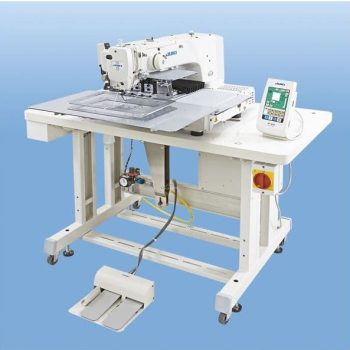
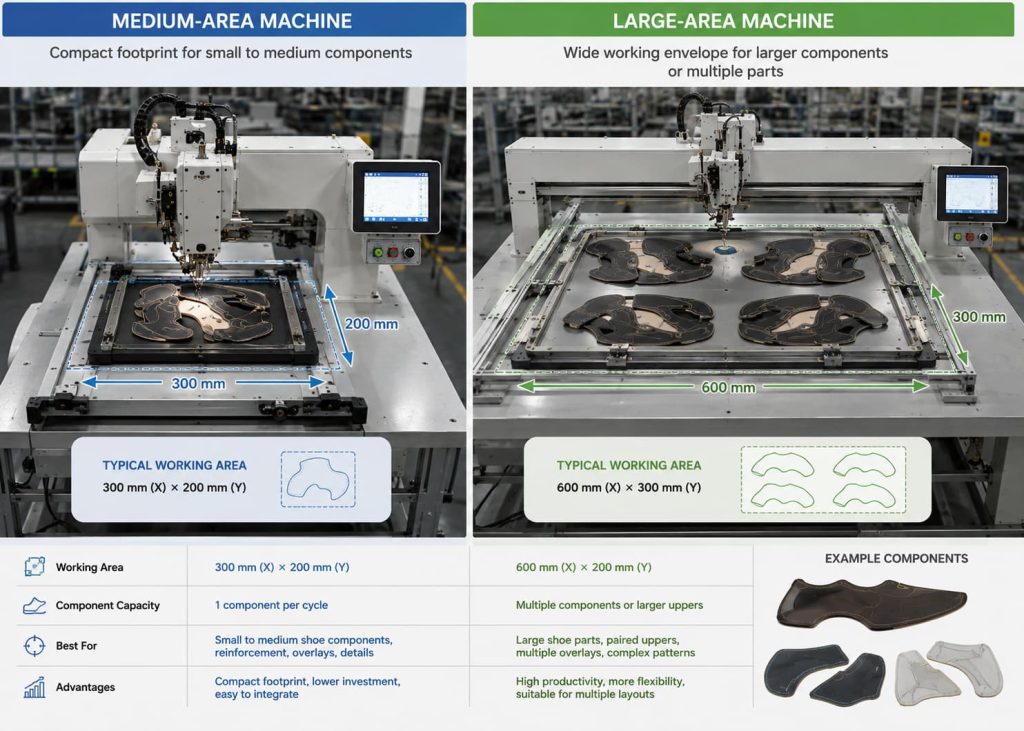
JUKI’s AMS-221EN Series provides a good example. JUKI offers configurations including the AMS-221EN-HS3020, with a 300 × 200 mm sewing area. JUKI identifies applications such as shape-tacking of boots and shoes, along with other products requiring a medium sewing area.
Therefore, when comparing machines, always check:
- actual sewing area;
- material capability;
- sewing speed;
- feeding-frame design;
- stitch length;
- hook capacity;
- programming functions;
- available fixtures.
The medium-area machine can provide a useful balance between flexibility, precision and production capacity.
Large-Area Computerized Stitching Machines
Large-area machines are useful when the footwear component, fixture or number of components requires a substantially larger working envelope. JUKI’s AMS-224EN Series provides an excellent manufacturer example. The series includes:
- AMS-224EN-4530: 450 × 300 mm sewing area
- AMS-224EN-6030: 600 × 300 mm sewing area
JUKI specifically lists applications including attaching parts to shoes and sports shoes and sewing a pair of shoes within the available area. The machine uses controlled X-Y feeding and is designed around productivity and energy efficiency.
This larger working area can allow a factory to:
- accommodate larger footwear components;
- position multiple small components;
- reduce repositioning;
- sew multiple pieces within one programmed cycle;
- improve fixture utilization.
Automatic and Multi-Pallet Computerized Stitching
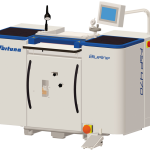
The next productivity improvement does not necessarily come from increasing sewing speed. It comes from reducing waiting time around the sewing operation. In a basic computerized machine, the operator loads the component, starts the cycle and waits until the machine completes the programmed operation. With a multi-pallet concept, one workpiece can be positioned or prepared while another is being stitched. This can help separate: Machine sewing time from Operator loading time.
The result can be better machine utilization, particularly in repetitive high-volume production. Golden Wheels CSA-3020XY/HAF (9053/9063N) demonstrates this broader productivity concept. Its system can automatically perform the programmed sewing and thread trimming, while optional equipment can allow an operator to attend to more than one machine in certain applications.
The actual benefit depends on the complete production cycle, including loading, unloading, pallet exchange and inspection.
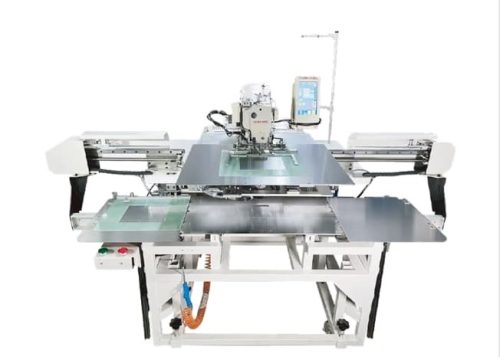
Computerized Stitching with Robotic Material Handling
The highest level of automation adds automatic material or pallet handling around the sewing machine. Here, the objective is not merely to automate the needle movement. The factory also attempts to automate the movement of workpieces between different stages of the sewing cycle. A typical concept is: Load → Automatic transfer → Programmed sewing → Automatic transfer → Next cycle
This can reduce:
- operator walking;
- manual pallet movement;
- machine waiting;
- repetitive handling;
- unnecessary operator movement.
However, robotic automation is normally justified only when the production volume and product stability support the investment. For highly variable footwear production, a flexible operator-operated computerized machine may actually be more practical than a fully automated cell.
Which Machine Type Gives Better Efficiency?
Efficiency should not be judged only by stitches per minute. A more useful footwear-production calculation considers the complete cycle:
| Efficiency Factor | Why It Matters |
|---|---|
| Sewing time | Direct machine productivity |
| Loading time | Operator utilization |
| Unloading time | Affects complete cycle |
| Pallet exchange | Determines machine waiting |
| Sewing area | Determines component capacity |
| Jig design | Controls positioning accuracy |
| Pattern change | Affects style flexibility |
| Quality/rejection | Determines usable output |
| Operator movement | Influences labour efficiency |
| Downtime | Reduces actual production |
For example, Brother’s BAS-326H can reach a published maximum sewing speed of 2,800 stitches/minute in the specified configuration, while JUKI’s AMS-224EN lists up to 2,500 stitches/minute. These numbers are useful specifications, but they do not by themselves determine pieces per hour. The actual cycle depends on the programmed pattern, stitch length, material, fixture, acceleration/deceleration and handling method.
Machine Selection for Footwear Factories
A practical selection approach is to match the machine to the production requirement.
| Production Requirement | Suitable Direction |
|---|---|
| Small repetitive component | Small-area programmable machine |
| Medium footwear component | Medium-area computerized machine |
| Larger component | Large-area computerized machine |
| Multiple components per cycle | Large-area machine + suitable fixture |
| High-volume repetitive production | Multi-pallet system |
| Stable high-volume operation | Automatic handling system |
| Highly repetitive dedicated operation | Dedicated automatic machine |
| High automation requirement | Robotic stitching cell |
Before purchasing, the factory should conduct a trial using the actual footwear upper, material, thread, stitch pattern and jig. This is important because catalogue specifications cannot predict every production result.
The Jig Is Part of the Machine System
In computerized footwear stitching, the jig or pallet is often as important as the sewing machine. A good fixture should consistently control:
- component position;
- orientation;
- seam allowance;
- material tension;
- stitch-line location;
- start and stop position.
If the component moves inside the fixture, the computerized machine may reproduce the programmed pattern accurately but still produce an incorrectly positioned seam
Therefore, real production performance is determined by: Machine + Program + Jig + Material + Operator Method, rather than the machine alone.
Conclusion
Computerized stitching machines have evolved from relatively simple programmable pattern machines into sophisticated production systems combining electronic sewing control, larger working areas, fixtures, multiple pallets and automated material handling.
For footwear manufacturers, the right machine should therefore be selected according to the operation, component size, production volume, cycle time, quality requirement and automation target.
The most expensive or most automated machine is not automatically the most efficient. The best computerized stitching system is the one that delivers the required quality with the lowest practical total production time and the right level of operator involvement.
FAQs – Frequently Asked Questions
It is an industrial sewing machine that uses programmed electronic controls to reproduce defined stitching patterns with controlled material movement.
Depending on machine capability, applications can include vamps, quarters, straps, tongues, decorative panels, logos, sports footwear components, leather components, and other repetitive stitching operations.
The primary advantage is repeatability. Once the program and production setup are validated, the machine can reproduce the same stitch path with considerably less operator-dependent variation.
It can reduce manual control and repetitive handling, but operators are still required for loading, inspection, setup, programming and production control.
Not necessarily. Complete cycle time also includes loading, unloading, thread trimming, pallet exchange and machine downtime.
Fixtures accurately locate and hold the footwear component. Poor positioning can produce incorrect stitch placement even when the computer-controlled machine itself is operating accurately.
Robotic stitching is most attractive for high-volume, stable and repetitive production where the reduction in manual handling can justify the additional investment.
The jig determines how accurately the footwear component is positioned. A good sewing program cannot compensate for a poorly positioned component.